ASSEMBLY
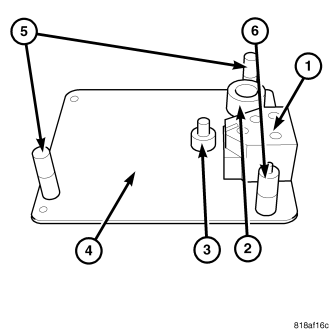
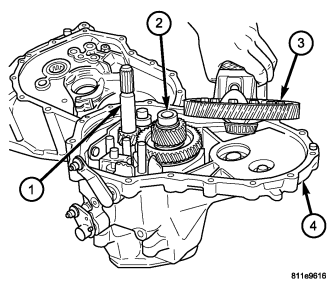
The T355 transaxle internal components can be serviced only by separating the gear case from the bellhousing case.
CAUTION: The transaxle output shaft is serviced as a unit. No disassembly and reassembly is possible. Damage to the transaxle may result.
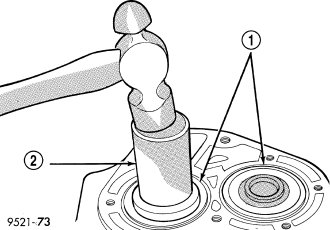
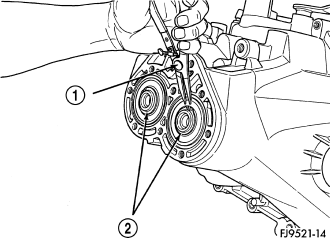
The sealant used to seal the transaxle case halves is MOPAR® Gasket Maker, Loctite® 518, or equivalent. The sealant used for the bearing end plate cover is MOPAR® RTV.
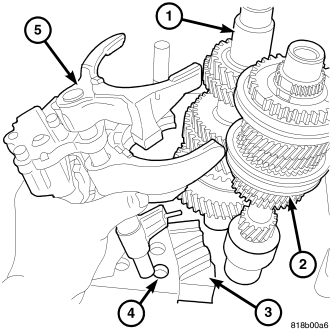
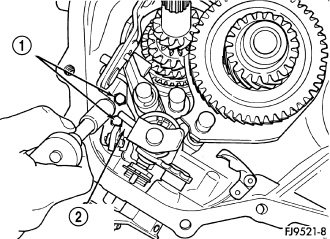
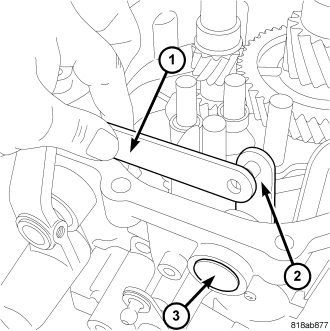
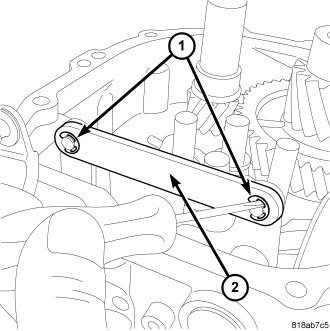
NOTE: Adaptor 9761-1 will slide shift blocker assembly and the 1-2 shift fork into the input and output shafts.
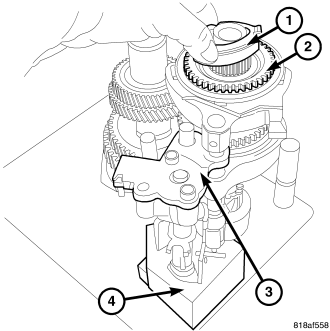
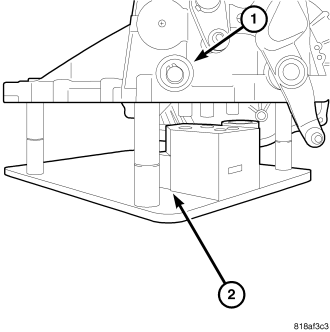
NOTE: One shift fork bolt may need to be installed to align assembly.
new
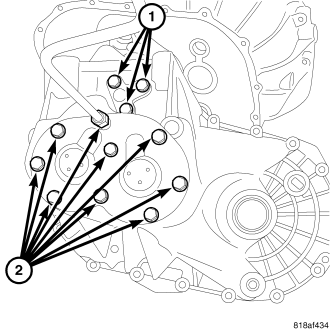
NOTE: Install new O-rings on shift blocker assembly bolts.
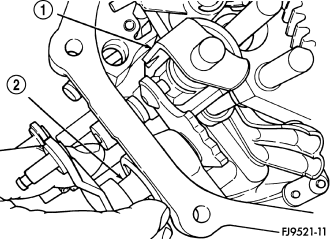
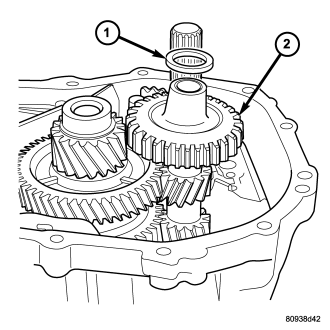
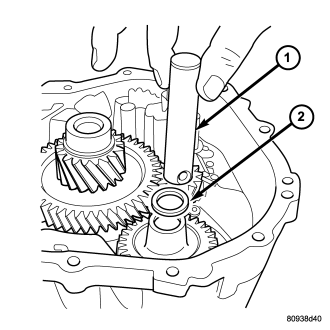
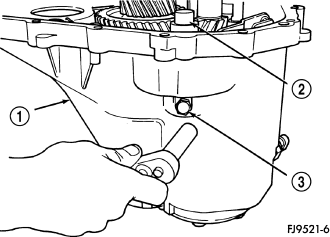
NOTE: Install a new O-ring on reverse idler shaft bolt.
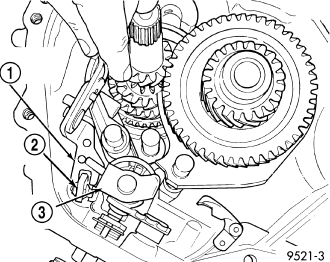
BEARING ADJUSTMENT PROCEDURE
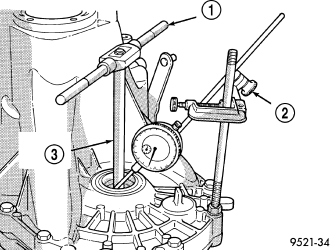
DIFFERENTIAL BEARING PRELOAD ADJUSTMENT
NOTE: True bearing turning–torque readings can be obtained only with the geartrain removed from the case.
NOTE: Position of dial indicator is for illustrative purposes only. The dial indicator should be parallel to T-Handle to obtain the most accurate reading.
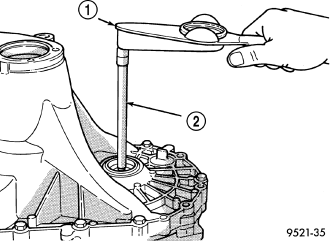
total of end play, plus (constant) preload of 0.18mm (0.007 in.).
The turning torque should be 6 to 12 in. lbs. If the turning torque is too high, install a 0.05 mm (0.002 inch) thinner shim. If the turning torque is too low, install a 0.05 mm (0.002 inch) thicker shim.
Once proper turning torque has been established, place gear case on the end plate. Draw a bead of MOPAR® Gasket Maker, Loctite® 518, or equivalent, on the flat surface of the case mating flange. Install clutch bellhousing onto gear case. Install and tighten case bolts to 25 N·m (225 in. lbs.).
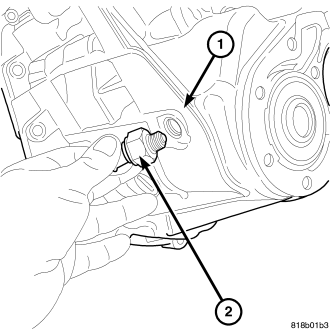

(Refer to 6 - CLUTCH/SLAVE CYLINDER - INSTALLATION)